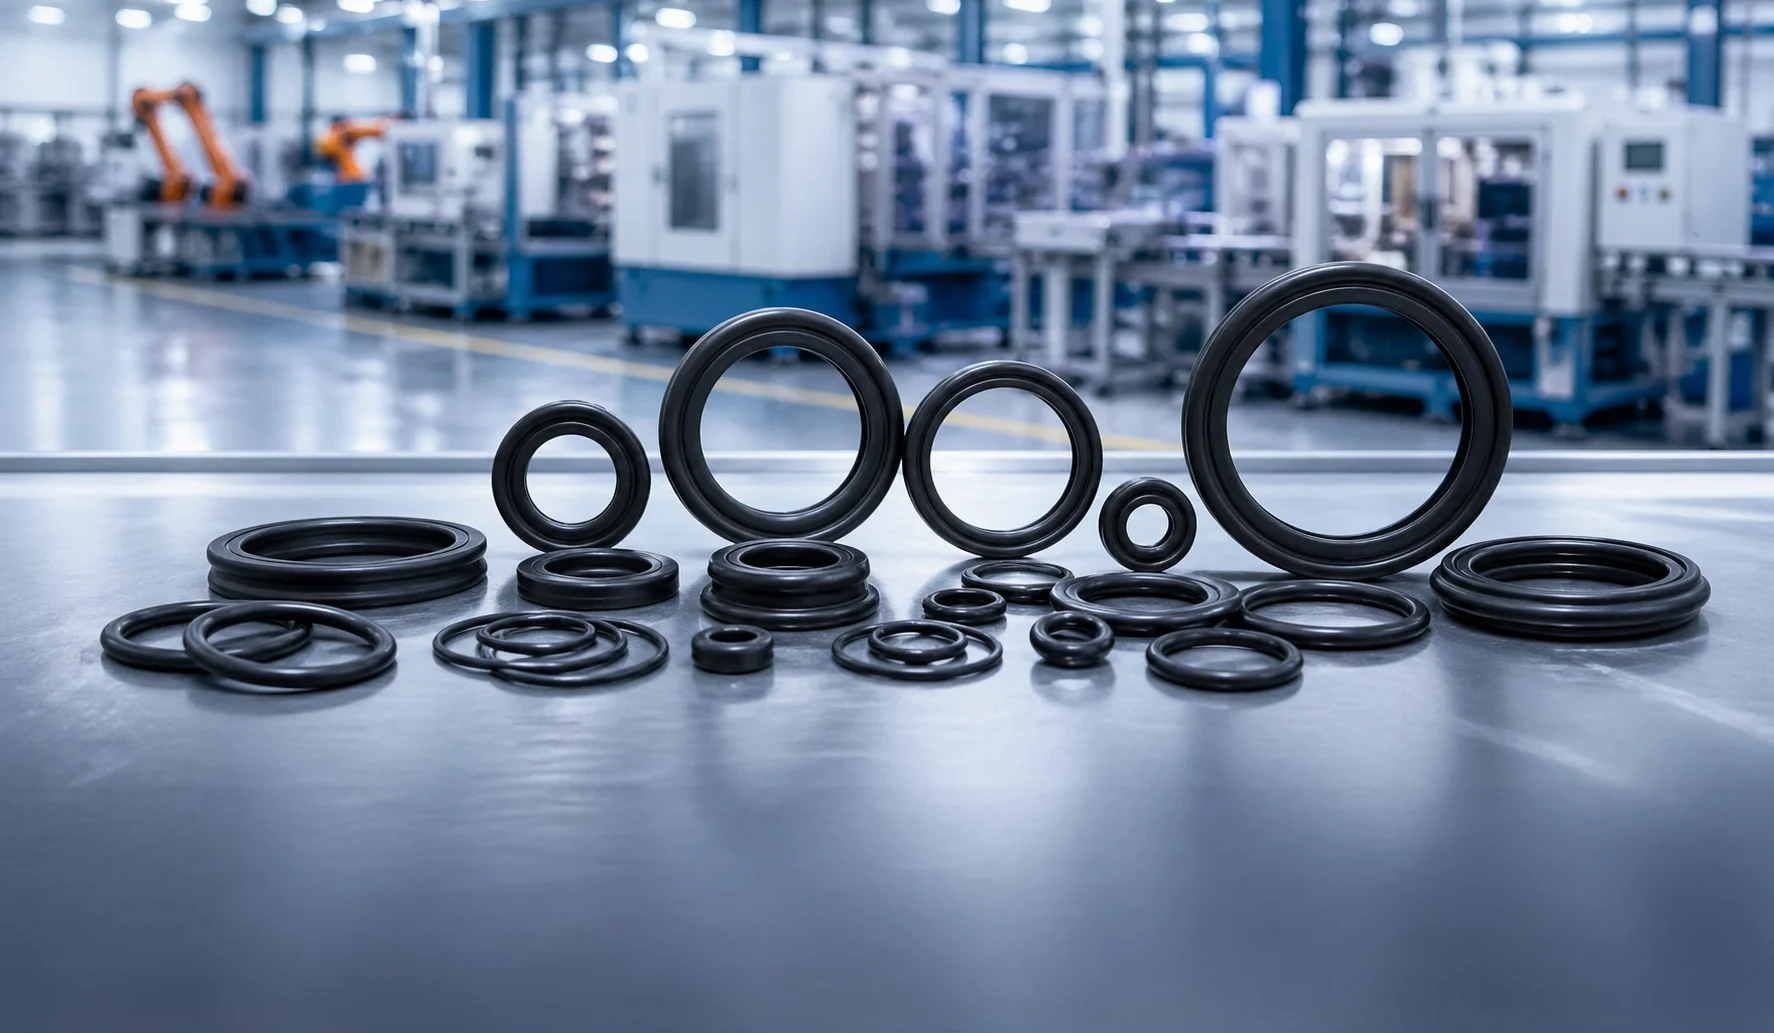
Hongjie Sealing Technology molds, extrudes, bonds, and die-cuts rubber and silicone parts to OEM drawings. Our Shenzhen facility has operated since 2001 and draws on 3,500+ existing tools and standard profiles. These resources help many orders avoid new mold costs and start production faster. Finished parts are exported to 45+ countries.
Twelve product lines run through the same certified tooling, molding, and inspection process:
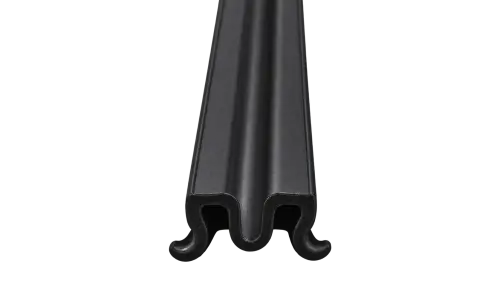
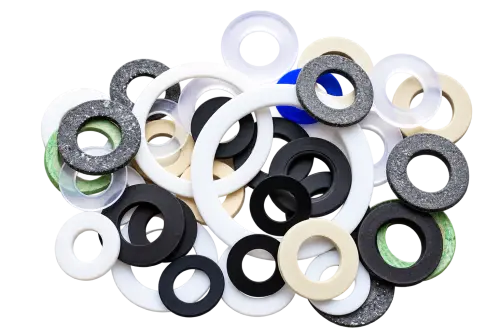
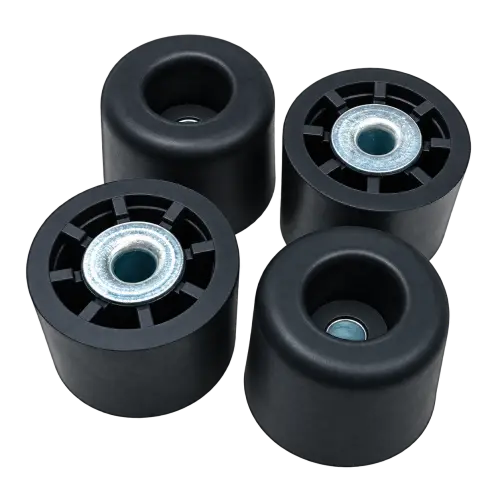
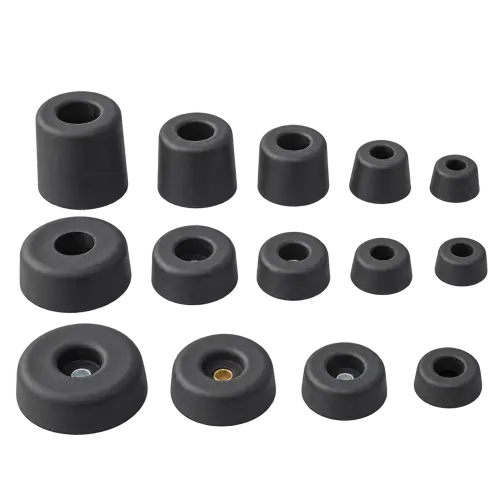

An 11,000 m² production facility supported by roughly 150 employees.

A 25-engineer design team with access to more than 200 proprietary rubber compounds.

IATF 16949:2016, ISO 13485:2016, and UL certification, with FDA/NSF-compliant material options.

More than 50 million precision-inspected parts supplied each year to global Tier-1 suppliers.

Injection molding and compression molding for custom rubber parts in different volumes, geometries, and cross-sections.

Extrusion, die-cutting, water-jet cutting, PSA lamination, and kiss-cutting.
Rubber-to-metal bonding and export-ready kitting for finished assemblies.
Injection molding suits high-cavity, tight-tolerance parts produced in volume. Compression molding is often more suitable for lower volumes or thick cross-sections when tooling cost needs to stay controlled.
The choice affects piece price, cavity count, and lead time. Our injection and compression molding guide explains how wall thickness and order volume influence the decision.
Parts that need a metal carrier or mounting stud are vulcanized directly onto a pre-treated insert during molding instead of being bonded afterward.
ON-TIME DELIVERY
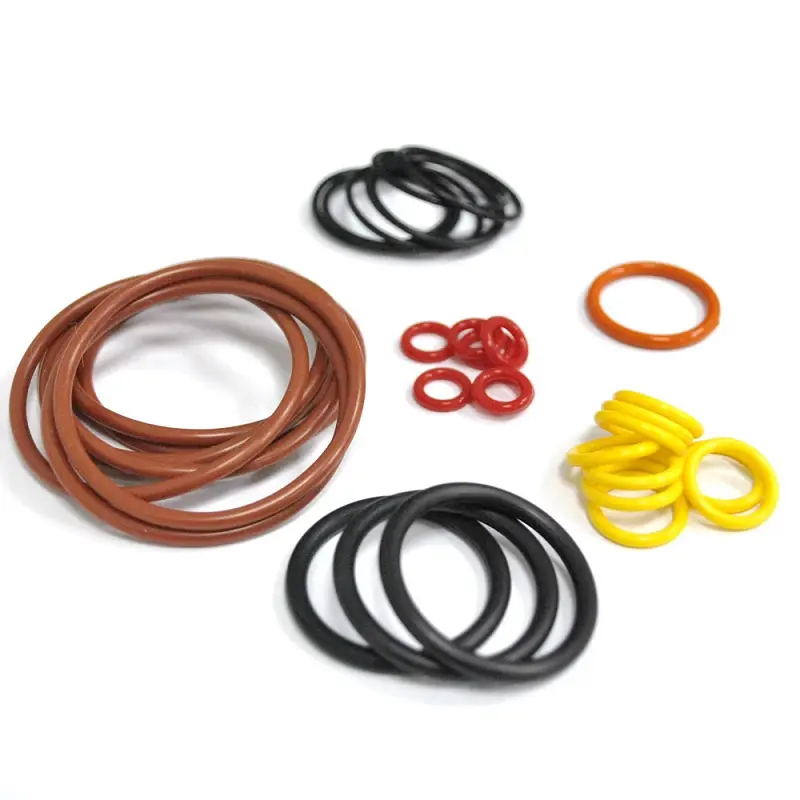
Available compounds include:
Temperature ratings range from –60°C to +325°C, with testing against more than 500 fluids and chemicals.
EPDM resists ozone and continuous steam exposure better than NBR, making EPDM rubber gaskets a practical starting point for outdoor enclosures and washdown equipment. Silicone covers a wide temperature range, while FKM/FFKM can extend service life where fuels or aggressive chemicals are present.
Dimensional control runs on two tiers, standard and precision, with the tightest tier holding to ±0.02mm on small features:
| Dimension Range | Standard | Precision |
|---|---|---|
| 0–10mm | ±0.10mm | ±0.02mm |
| 10–25mm | ±0.15mm | ±0.05mm |
| 25–50mm | ±0.20mm | ±0.08mm |
| 50–100mm | ±0.25mm | ±0.10mm |
Production targets Cpk > 1.33 under SPC and Six Sigma monitoring, backed by IATF 16949, ISO 13485, UL, FDA, and NSF compliance. Pick the tolerance tier the assembly actually needs, not the tightest one available — rubber shifts more across cure and post-shrink than metal or plastic, so an oversized tolerance budget just adds inspection cost without improving fit.
Automotive diaphragm programs requiring PPAP documentation use the tooling validated during prototyping. This helps maintain the approved geometry through volume production without a separate re-tooling step.
More than 3,500 profiles are available, allowing many suitable parts to move directly into sampling without new-mold development.
Engineers work from 3D CAD and FEA models in STEP or IGES format. Functional prototypes typically take 3–5 business days.
Costs scale with cavity count and part complexity. Single-cavity die-cut parts sit at the low end, while multi-cavity injection-molded assemblies with metal inserts sit at the high end.
Lead time increases with cavity count and order volume after design sign-off.
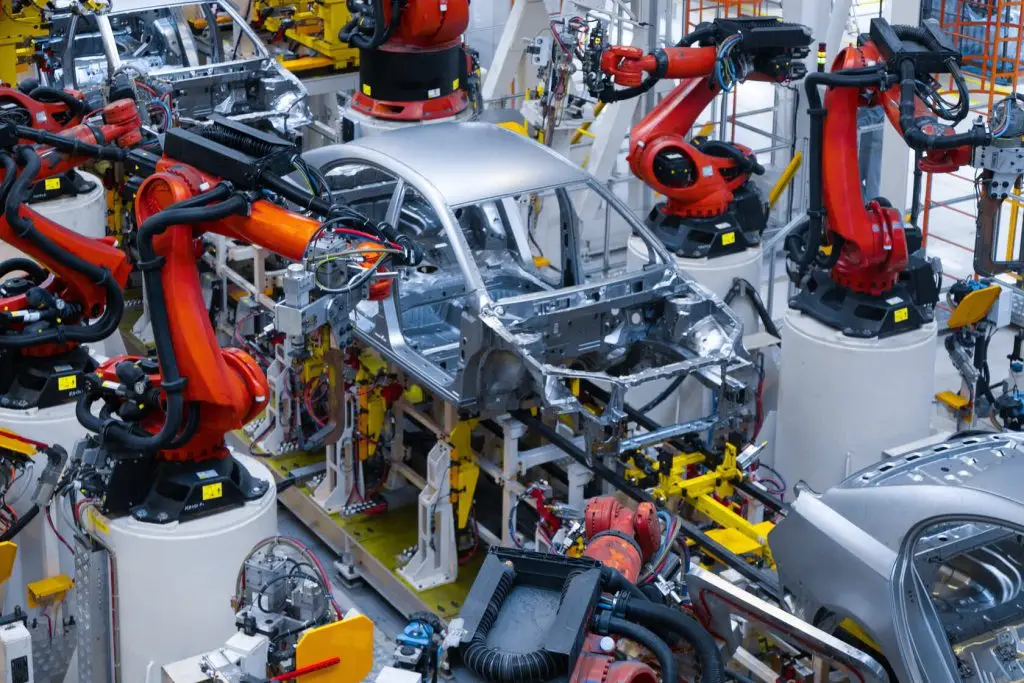
Parts ship into automotive, medical, appliance, hydraulic, and general industrial programs, with a smaller volume of aerospace work. Certification and compound selection are matched to the sector — FDA/NSF materials for medical and food-adjacent parts, oil- and fuel-resistant compounds for hydraulic and automotive sealing.
One limitation worth flagging before sending a drawing: Hongjie molds, extrudes, bonds, and die-cuts rubber and silicone components only. Metal-only stampings, plastic-only housings, and hardware outside a rubber-to-metal bonded assembly fall outside what gets manufactured here.
Vibration-isolation and mounting applications are handled under custom rubber bushings.
Our engineering team reviews your specs and responds within 24 hours with material recommendations and competitive pricing.